Meibao Environmental Protection Equipment Co., Ltd. was established on July 1, 2016, in Nanyang, Henan Province. With a 85,000m² production base, we have grown into China's largest plastic pump manufacturer, specializing in R&D, production, and sales of corrosion-resistant pumps, filters, and fans.
Our product portfolio spans 13 series and 1,000+ models — including idling self-priming pumps, magnetic pumps, chemical centrifugal pumps, vertical pumps, fluorine-lined pumps, dosing pumps, diaphragm pumps, submersible pumps, filters, and FRP fans. Trusted by 28,000+ enterprises, our products are exported to 50+ countries and regions worldwide.
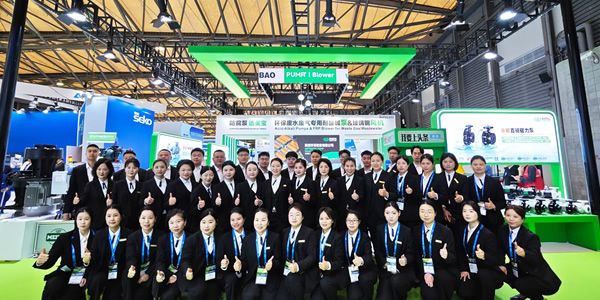
To engineer and manufacture industrial pumps that deliver maximum reliability, efficiency, and value | enabling our clients across the world to process fluids safely, cost-effectively, and without interruption. We believe every facility deserves access to world-class pump technology at a fair price.
To be the most trusted and respected industrial pump brand in the global market | recognized for innovation, quality, and customer partnership. By 2030, Meibao aims to be the preferred pump supplier for Fortune 500 manufacturing operations worldwide.
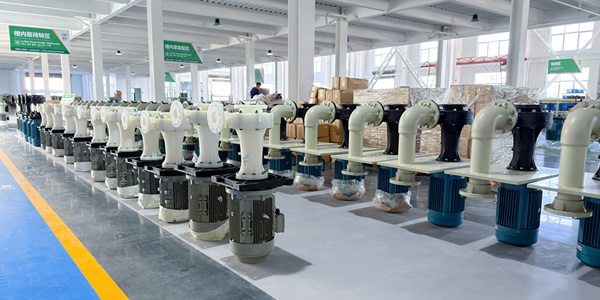
Our integrated manufacturing ecosystem spans 8.33 hectares, ensuring consistent quality, competitive pricing, and reliable supply for clients worldwide.
Explore our 8.33-hectare manufacturing complex, R&D center, and quality control labs — all in an interactive virtual tour.
ISO 9001:2015 certified, our quality management system governs every step from raw material procurement to final inspection and packaging.
Every batch of metal, polymer, and sealing material is tested for composition, hardness, and chemical resistance before entering production.
Statistical process control at every critical machining step. Dimensional tolerances verified with CMM and laser measurement systems.
100% of pumps undergo hydraulic performance testing. Flow, head, power consumption, and NPSH curves plotted against catalog specifications.
Final dimensional check, hydrostatic pressure test, noise/vibration measurement, and export-grade packaging with anti-corrosion treatment.


From a single workshop in Nanyang to 19 branches worldwide and 50+ countries — our history reflects relentless innovation, strategic expansion, and unwavering commitment to quality in corrosion-resistant pump technology.
Every business decision is guided by engineering logic. We invest in R&D before marketing, in quality before quantity, and in long-term reliability over short-term cost.
We treat every client inquiry as the beginning of a long-term partnership, not a transaction. Our sales engineers are technically trained to understand your process before recommending a solution.
Kaizen philosophy embedded in our operations. Every month we review defect rates, customer feedback, and process inefficiencies | driving incremental improvements that compound over time.
Our products travel to 50+ countries, and so does our thinking. We design to international standards, communicate across time zones, and adapt our solutions to local industrial norms.
Energy-efficient pump design is central to our R&D. Our magnetic drive and variable frequency pump lines help clients reduce energy consumption by up to 30% versus traditional designs.
What we promise, we deliver. On-time, in full, with the right documentation. Our logistics team maintains a 97%+ on-time delivery rate and traces every shipment in real time.
We welcome clients and partners to tour our production facilities in Nanyang. Schedule a factory visit or request a virtual walkthrough with our export team.
 WhatsApp
 Facebook
 LinkedIn
 YouTube
