Corrosion-Resistant Vertical Pump for Scrubber Systems: 520 L/min Stable Spray Pressure, 6+ Months Zero Cavitation Failure
How a Russian waste gas treatment facility eliminated pump motor corrosion, cavitation damage, and 18 days of annual downtime by switching to PPH vertical pumps for acid-base washing solution circulation
Meibao vertical pumps provide stable corrosion resistance and rarely leak during continuous operation. The vertical structure keeps the motor above the liquid surface, effectively protecting it from corrosive mist. Unlike horizontal pumps, they do not draw in air when the liquid level changes, which helps prevent cavitation and unstable spray pressure. Compared with other brands we have tried, they require much less maintenance and greatly reduce equipment downtime.
Corrosion-Resistant Vertical Pump for Scrubber Systems: 520 L/min Stable Spray Pressure, 6+ Months Zero Cavitation Failure
How a Russian waste gas treatment facility eliminated pump motor corrosion, cavitation damage, and 18 days of annual downtime by switching to PPH vertical pumps for acid-base washing solution circulation Customer Testimonial
Act 1: The Challenge —— Double Corrosion from Acid and Alkali Mist, Plus Cavitation from Changing Liquid Levels
Background
Moscow Industrial Waste Gas Treatment Engineering Co. is a professional industrial waste gas treatment company in Russia. It provides scrubber system design, installation, and maintenance services for industrial customers. Its scrubber systems use an alternating acid and alkaline spray process: diluted sulfuric acid (H₂SO₄) is used to treat alkaline waste gas, while sodium hydroxide (NaOH) solution is used to treat acidic waste gas. The spray liquid circulates between the collection tank at the bottom of the tower and the spray nozzles at the top, removing harmful gases through gas-liquid contact and neutralization.
The customer operates 5 scrubber systems, with one circulation pump for each system. The pumps must run continuously to maintain stable waste gas treatment performance. The scrubber systems are usually installed outdoors or in semi-open areas. During the Russian winter, ambient temperatures can drop below -20°C, while the washing solution can reach 50°C. This large temperature difference increases thermal expansion and contraction, which can accelerate seal aging.
However, this seemingly simple circulation system had become one of the most troublesome parts of the entire scrubber system.
Key Problems
The horizontal pumps previously used by the customer had several serious problems:
- Acid and alkaline mist corrosion: The scrubber system contains both acidic waste gas and alkaline spray liquid. The horizontal pump motors and bearings were exposed to acid and alkaline mist for long periods, causing electrical insulation aging and bearing corrosion.
- Frequent cavitation: The liquid level in the scrubber collection tank changed frequently due to water supply, drainage, and evaporation. When the liquid level dropped, the horizontal pumps could draw in air and cause cavitation. This caused unstable flow and spray pressure, directly affecting waste gas treatment performance, while also damaging the impeller and shortening pump life.
- Repeated leakage: Mechanical seals aged quickly in the alternating acid and alkaline environment, causing 2–3 leakage incidents every year. Acid and alkaline solution leaks created serious safety and environmental risks.
- High downtime losses: Pump failures forced the scrubber systems to reduce operation or stop. In some cases, the waste gas treatment system had to operate at a lower load or bypass the process, creating a high environmental compliance risk. Annual downtime reached 18 days.
The average pump life was only 12 months, while the total annual cost per set reached $520, including purchase, maintenance, and downtime losses.
Highlight Box — Root Cause Analysis
Root Causes
1. Double corrosion environment: Acidic waste gas and alkaline spray liquid existed in the same scrubber system. The horizontal pump motor was exposed to alternating acid and alkaline mist.
2. Large liquid-level changes: The collection tank level changed frequently due to water supply, drainage, and evaporation, causing poor suction and cavitation in the horizontal pump.
3. Cavitation damage cycle: Cavitation → impeller damage → lower flow → unstable spray pressure → unstable treatment performance → faster pump failure.
4. Horizontal pump structure: The mechanical seal aged quickly in the alternating acid and alkaline environment, causing repeated leakage.
5. Cold climate: The harsh Russian winter increased thermal expansion and contraction, accelerating seal aging and material embrittlement.
Before Data
Metric | Before Meibao | Impact |
Pump Lifespan | 1 year average | Annual replacement across 5 scrubber systems |
Annual Downtime | 18 days/year | ~3.5 production weeks lost, emission compliance risk |
Leakage Incidents | 2–3 times/year | Acid-base spills, EHS risk |
Annual Equipment Cost | $520/set | Purchase + labour + downtime |
Wash Solution Concentration | 10% | H₂SO₄ + NaOH spray liquid |
Operating Temp | 50°C | Accelerates corrosion and seal aging |
Ambient Temp (Winter) | Below -20°C | Thermal shock, seal brittleness |
Cavitation Frequency | Frequent during level fluctuation | Impeller damage, pressure instability |
Act 2: The Solution —— PPH Vertical Pumps Solve Both Cavitation and Corrosion Problems
Solution Approach
The main problem seemed to be that the pumps failed too often. But after a detailed review, we found that the real problem was the mismatch between the horizontal pump design and the scrubber operating conditions:
- Liquid-level changes are a normal part of scrubber operation and cannot be completely avoided → horizontal pumps are more likely to suffer from poor suction and cavitation.
- Acid and alkaline mist are always present during scrubber operation → horizontal pump motors remain exposed to the corrosive environment.
- The harsh Russian winter makes equipment aging worse → a more weather-resistant and simpler pump design is needed.
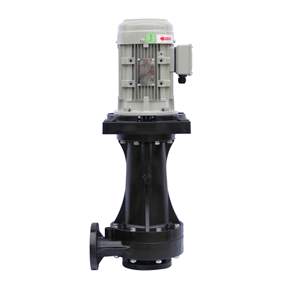
The solution was not simply to find a "more corrosion-resistant horizontal pump." Instead, we selected a pump type that naturally fits scrubber operating conditions. The vertical pump uses a submerged installation, so changing liquid levels have less impact on suction. The motor stays above the liquid surface and away from acid and alkaline mist. Its seal-less design also removes the main leakage point.
The customer accepted our recommendation and replaced all 5 scrubber pumps with MIT-50VK-75NF vertical pumps.
Product Selection
Selection Factor | MIT-50VK-75NF Matching Advantage |
Vertical Structure | Motor stays above the liquid surface and away from acid and alkaline mist |
Submerged Impeller | Impeller stays below the liquid surface, helping prevent air intake and cavitation when the liquid level changes |
PPH Wetted Material | Resistant to alternating 10% H₂SO₄ + NaOH spray liquid at 50°C |
Seal-less Design | Eliminates mechanical seal leakage, suitable for alternating acid and alkaline conditions |
High Flow and Head | 520 L/min + 24 m head for stable spray pressure |
Simple Structure | Fewer seals and wear parts, improving reliability in cold environments |
Highlight Box — Key Technical Advantages
Vertical Structure · Cavitation Protection · Zero Leakage
Motor away from acid and alkaline mist: The vertical design keeps the motor naturally above the liquid surface, reducing exposure to corrosive mist.
Cavitation protection: The submerged impeller stays below the liquid surface. Even when the scrubber liquid level changes, it maintains stable suction and helps prevent air intake and cavitation.
Zero-leakage design: No mechanical shaft seal, eliminating the main path for acid and alkaline liquid leakage.
PPH all-plastic flow path: Resistant to alternating H₂SO₄ and NaOH spray liquid.
Cold-weather suitability: The simple structure and fewer sealing parts improve reliability in the harsh Russian winter environment.
Specification Table
Specification | Selected Model (MIT-50VK-75NF) | Key Benefit |
Wet-End Material | PPH (Polypropylene) | Corrosion-resistant to H₂SO₄ + NaOH spray liquid |
Drive Type | Vertical direct drive | No shaft seal, zero leakage |
Max Flow | 520 L/min | Stable circulation to scrubber spray headers |
Max Head | 24 m | Maintains stable spray pressure |
Motor Rating | 5.5 kW | Adequate power margin for high head |
Units Installed | 5 units | Full coverage for all scrubber systems |
Sealing | Seal-less (vertical submerged) | No wear parts, no leakage |
Certification | None required | Standard industrial specification |
Project Timeline
Stage | Timeline | Description |
Application Assessment | Week 1–2 | On-site review of 5 scrubber systems, liquid-level changes, and piping layout |
Custom Production | Week 3–5 | 5 MIT-50VK-75NF pumps customized to the customer's connections and fully inspected before shipment |
Installation & Testing | Week 6–7 | On-site installation, piping connection, system testing, and variable-level operation tests |
Stable Operation | Month 6+ | Continuous failure-free operation to date, including the Russian winter, with ongoing monitoring |
Act 3: The Result —— Zero Cavitation, Zero Leakage, Stable Spray Pressure
Results
Since installation and commissioning were completed in January 2026, the 5 MIT-50VK-75NF vertical pumps have operated continuously on the customer's scrubber systems for more than 6 months, including the harsh Russian winter. During this period, all pumps achieved zero leakage, zero cavitation, and zero downtime:
- Cavitation eliminated: Even when the scrubber collection tank liquid level changed frequently due to water supply and drainage, the submerged impeller maintained stable suction. The pumps continued to deliver 520 L/min at 24 m head, keeping spray pressure stable and waste gas treatment performance consistent.
- Motor protection: The vertical structure keeps the motor away from the acid and alkaline mist. After 6 months of operation, there were no visible signs of corrosion on the motor housing or internal insulation.
- Cleaner working environment: With zero leakage, the area around the scrubber systems remained dry, greatly reducing the risk of acid and alkaline solution contamination.
Technical Director Ivan Petrov highlighted that the vertical pump design solved the cavitation problem caused by air entering horizontal pumps when the liquid level changed. This had been one of the most common pump failure modes in their scrubber systems. Compared with other brands they had tried, Meibao pumps required much less maintenance and significantly reduced equipment downtime.
Results Cards
✓ | $ | 🛡️ |
6+ mo | $350 | 0 |
Zero-downtime continuous operation | Annual cost saving per set vs. previous pumps | Leakage incidents across all 5 units |
No cavitation, stable spray pressure | No motor corrosion |
Before vs. After
Comparison | Before (Previous Horizontal Pumps) | After (MIT-50VK-75NF) | Improvement |
Motor Corrosion | Acid and alkaline mist caused insulation aging and failure within 6–12 months | Motor stays above the liquid surface, with no visible corrosion after 6 months | Expected service life extended 2–3× |
Cavitation | Frequent cavitation when the liquid level changed, causing impeller damage | Submerged installation prevents air intake when the liquid level changes | Eliminated |
Spray Pressure | Large fluctuations, causing unstable treatment performance | Stable throughout operation | Stable waste gas treatment performance |
Leakage Incidents | 2–3 times/year | 0 | Leakage eliminated |
Production Downtime | 18 days/year | 0 days | 3.5 weeks of production recovered |
Annual Total Cost | $520/set (purchase + maintenance + downtime losses) | Initial investment only, with very low operating cost | Annual savings of $350+/set |
Recommended Pumps for
Corrosion-Resistant Vertical Pump for Scrubber Systems: 520 L/min Stable Spray Pressure, 6+ Months Zero Cavitation Failure
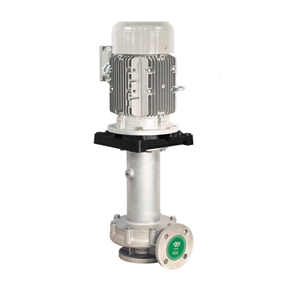
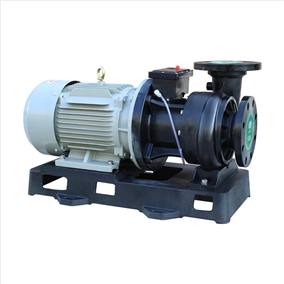
Each pump model is available in multiple material configurations to match the exact chemical and thermal requirements of your process.
 Recommended
 Recommended
 Recommended
 Recommended
Get a Free Technical Proposal
Tell us about your HF acid, chemical, or corrosive media application. Our engineering team will recommend the right pump and provide a detailed proposal within 48 hours.
 WhatsApp
 Facebook
 LinkedIn
 YouTube
