Meibao Environmental Protection Equipment Co., Ltd. được thành lập vào ngày 1 tháng 7 năm 2016, ở Nam Dương, tỉnh Hà Nam. Với 85.000m & sup2; cơ sở sản xuất, chúng tôi đã phát triển thành nhà sản xuất bơm nhựa lớn nhất của Trung Quốc, chuyên về R & D, sản xuất và bán máy bơm chống ăn mòn, bộ lọc và quạt.
Danh mục sản phẩm của chúng tôi trải dài 13 loạt và 1.000 mô hình bao gồm máy bơm tự lấp, máy bơm từ tính, máy bơm ly tâm hóa học, máy bơm dọc, máy bơm được lót fluor, máy bơm liều lượng, máy bơm màng, máy bơm chìm, bộ lọc và quạt FRP. Được tin tưởng bởi 28.000 doanh nghiệp, sản phẩm của chúng tôi được xuất khẩu đến 50 quốc gia và khu vực trên toàn thế giới.
To engineer and manufacture industrial pumps that deliver maximum reliability, efficiency, and value | enabling our clients across the world to process fluids safely, cost-effectively, and without interruption. We believe every facility deserves access to world-class pump technology at a fair price.
To be the most trusted and respected industrial pump brand in the global market | recognized for innovation, quality, and customer partnership. By 2030, Meibao aims to be the preferred pump supplier for Fortune 500 manufacturing operations worldwide.
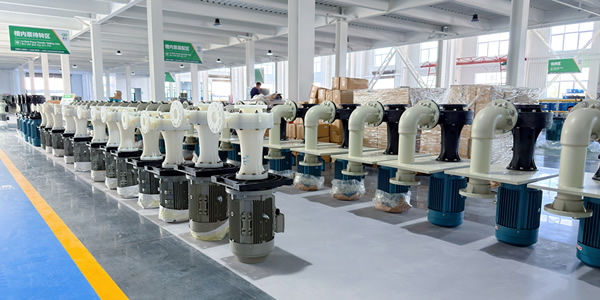
Our integrated manufacturing ecosystem spans 8.33 hectares, ensuring consistent quality, competitive pricing, and reliable supply for clients worldwide.
Explore our 8.33-hectare manufacturing complex, R&D center, and quality control labs — all in an interactive virtual tour.
ISO 9001:2015 certified, our quality management system governs every step from raw material procurement to final inspection and packaging.
Every batch of metal, polymer, and sealing material is tested for composition, hardness, and chemical resistance before entering production.
Statistical process control at every critical machining step. Dimensional tolerances verified with CMM and laser measurement systems.
100% of pumps undergo hydraulic performance testing. Flow, head, power consumption, and NPSH curves plotted against catalog specifications.
Final dimensional check, hydrostatic pressure test, noise/vibration measurement, and export-grade packaging with anti-corrosion treatment.


From a single workshop in Nanyang to 19 branches worldwide and 50+ countries — our history reflects relentless innovation, strategic expansion, and unwavering commitment to quality in corrosion-resistant pump technology.
Every business decision is guided by engineering logic. We invest in R&D before marketing, in quality before quantity, and in long-term reliability over short-term cost.
We treat every client inquiry as the beginning of a long-term partnership, not a transaction. Our sales engineers are technically trained to understand your process before recommending a solution.
Kaizen philosophy embedded in our operations. Every month we review defect rates, customer feedback, and process inefficiencies | driving incremental improvements that compound over time.
Our products travel to 50+ countries, and so does our thinking. We design to international standards, communicate across time zones, and adapt our solutions to local industrial norms.
Energy-efficient pump design is central to our R&D. Our magnetic drive and variable frequency pump lines help clients reduce energy consumption by up to 30% versus traditional designs.
What we promise, we deliver. On-time, in full, with the right documentation. Our logistics team maintains a 97%+ on-time delivery rate and traces every shipment in real time.
We welcome clients and partners to tour our production facilities in Nanyang. Schedule a factory visit or request a virtual walkthrough with our export team.
 WhatsApp
 Facebook
 LinkedIn
 YouTube
