AAL Electroplating Pickling Case Study
Zero-Leakage Vertical Pickling Pump: 450 L/min, 7+ Months of Continuous Operation
Meibao pumps provide stable corrosion resistance and rarely leak during continuous operation. Compared with other brands, they need much less maintenance and have significantly reduced production downtime.
From Three Major Leakage Incidents to 36 Months of Bulletproof HF Transfer
Viet Semiconductor Components JSC operates a 200mm wafer fabrication facility in Ho Chi Minh City, Vietnam, processing 12,000 litres of hydrofluoric acid daily for silicon wafer etching. A history of pump failures and toxic HF leakage incidents made this one of Meibao's most demanding | and most rewarding | installation projects.
AAL is an electroplating company in India. Its pickling process uses a 20% hydrochloric acid and sulfuric acid mixture at 60°C to remove oxide from metal surfaces.
The pickling tanks continuously circulate the acid solution through filter machines to keep the bath clean. However, the open tanks release corrosive acid fumes into the workshop. At the same time, the acid contains a large amount of iron oxide sludge, creating both chemical corrosion and particle wear inside the pump.
The Problems
Before working with Meibao, AAL had tried several pump brands, but none could provide stable operation under these conditions.
The main problems included:
- Acid fumes attacked the motor and bearings.
- Iron oxide particles caused wear on the impeller and pump casing.
- The average pump service life was only about 12 months.
- Pump failures caused repeated repairs and replacements.
- Production downtime reached around 15 days per year.
- Acid leakage occurred 2–4 times per year, creating safety and EHS concerns.
The customer needed more than a pump with better corrosion resistance. The solution also had to address acid-fume exposure, leakage, and changing tank levels.
Root Cause
Why were the previous pumps failing?
1. Acid-fume exposure
Open pickling tanks continuously released HCl + H₂SO₄ fumes. Horizontal pumps left the motor and bearing area exposed to the corrosive environment.
2. Corrosion + particle wear
The 20% mixed acid attacked wetted components, while iron oxide sludge accelerated mechanical wear.
3. Shaft-seal leakage
The shaft seal became a weak point under corrosive conditions, leading to repeated acid leakage.
4. Tank-level changes
Changes in liquid level could make the horizontal pump more likely to lose stable suction conditions, increasing the risk of cavitation.
Before Meibao
Metric | Before Meibao | Impact |
Pump Lifespan | About 1 year | Frequent replacement |
Annual Downtime | 15 days/year | About 2 weeks of production lost |
Leakage Incidents | 2–4 times/year | EHS and operator safety concerns |
Annual Pump Cost | $500/set | Purchase + labor + downtime |
Acid Concentration | 20% | HCl + H₂SO₄ mixed acid |
Operating Temperature | 60°C | Increased corrosion and seal wear |
A Vertical Pump with PPH Wetted Parts
After reviewing AAL's actual operating conditions, Meibao identified three key requirements:
Keep the motor away from acid fumes. Prevent shaft-seal leakage. Maintain stable operation when the tank level changes.
A conventional horizontal pump could not fully address these issues.
Meibao therefore recommended the MIT-40VK-55NF vertical pump.
Its vertical design places the motor above the liquid level, while the seal-less structure removes the traditional shaft-seal leakage point. PPH wetted parts were selected for the customer's mixed-acid application and 60°C operating temperature.
Why MIT-40VK-55NF?
Selection Requirement | MIT-40VK-55NF Advantage |
Acid-fume exposure | Motor is positioned above the liquid level and away from the main fume area |
Corrosive liquid | PPH wetted parts are designed for corrosive chemical service |
Leakage prevention | Seal-less design removes the mechanical shaft-seal leakage point |
Changing liquid levels | Vertical submerged pump design helps maintain stable liquid intake |
Circulation flow | Up to 450 L/min for filter-machine circulation |
Key Advantages
Vertical Design · Seal-Less Structure · Stable Operation
· Motor away from acid fumes: The vertical design keeps the motor above the liquid level, reducing exposure to corrosive fumes.
· No shaft-seal leakage: The seal-less design removes a common leakage point found in conventional shaft-seal pumps.
· Better handling of changing liquid levels: The submerged pump section stays in the liquid, helping maintain stable suction as the tank level changes.
· PPH wetted parts: The wetted components are made from PPH for corrosion resistance in the customer's mixed-acid application.
Selected Pump Specifications
Specification | MIT-40VK-55NF | Key Benefit |
Wetted Material | PPH | Corrosion-resistant wetted parts |
Drive Type | Vertical direct drive | Seal-less pump design |
Max. Flow | 450 L/min | Stable circulation to filter machines |
Max. Head | 21 m | Handles system back pressure |
Motor Power | 3.75 kW | Suitable for the application |
Units Installed | 6 | Covers the customer's pickling system |
Sealing | Seal-less | No mechanical shaft seal |
Certification | None required | Standard industrial application |
Project Timeline
Stage | Timeline | What Happened |
Application Review | Week 1–2 | Reviewed the pickling process, liquid-level changes, and piping layout |
Production & Testing | Week 3–5 | Six MIT-40VK-55NF pumps were customized to match the customer's connections and fully inspected before shipment |
Installation & Commissioning | Week 6–7 | Pumps were installed, connected, tested, and commissioned under load |
Stable Operation | Month 7+ | Pumps have continued running without failure and are still being monitored |
Zero Leakage and Stable Operation for 7+ Months
Since installation and commissioning were completed in November 2025, all six MIT-40VK-55NF vertical pumps have operated continuously for more than 7 months in AAL's pickling workshop.
During this period:
| 0 leakage | incidents |
| 0 days of | production downtime caused by the pumps |
| Stable | circulation of up to 450 L/min |
| No pump failures | requiring replacement |
| Significantly | less maintenance compared with the previous pumps |
The vertical design also keeps the motor above the liquid level, reducing its exposure to the acid-fume environment.
At the same time, the seal-less design removes the shaft-seal leakage point, helping keep the working area cleaner and reducing EHS concerns related to acid leakage.
Customer Feedback
“Meibao pumps provide stable corrosion resistance and rarely leak during continuous operation. Compared with other brands, they need much less maintenance and have significantly reduced production downtime.”
— Patel, Director, AAL
Recommended Pumps for
AAL Electroplating Pickling Case Study
Each pump model is available in multiple material configurations to match the exact chemical and thermal requirements of your process.
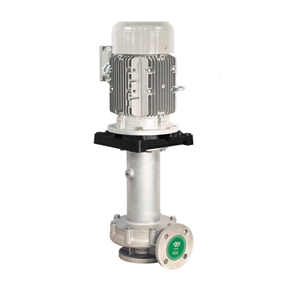 Recommended
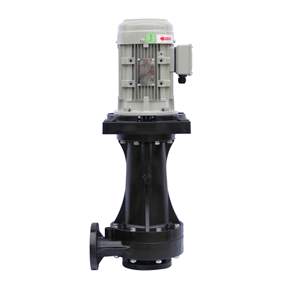 Recommended
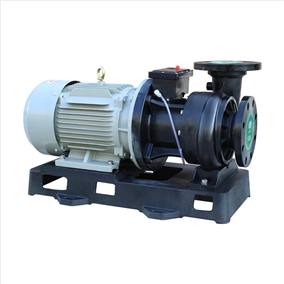 Recommended
 Recommended
Related Case Studies
Get a Free Technical Proposal
Tell us about your HF acid, chemical, or corrosive media application. Our engineering team will recommend the right pump and provide a detailed proposal within 48 hours.
 WhatsApp
 Facebook
 LinkedIn
 YouTube
