Complete Pre-Treatment Solution: MIT Vertical Pumps + TF FRP Fans Deliver 16+ Months of Zero-Leakage, Zero-Downtime Operation
How a Malaysian electrocoating facility eliminated corrosive alkaline/acid fumes and frequent maintenance across its degreasing and pickling lines with Meibao's integrated pump and exhaust system
Meibao MIT in-tank vertical pumps deliver outstanding corrosion resistance and barely leak under non-stop continuous operation. Other pump brands we have used in the past required regular maintenance; Meibao units greatly reduce service interruptions. Paired with Meibao TF FRP centrifugal fans, the whole exhaust system runs reliably. The combined MIT pump and TF fan solution keeps our entire pre-treatment process running steadily.
Complete Pre-Treatment Solution: MIT Vertical Pumps + TF FRP Fans Deliver 16+ Months of Zero-Leakage, Zero-Downtime Operation
How a Malaysian electrocoating facility eliminated corrosive alkaline/acid fumes and frequent maintenance across its degreasing and pickling lines with Meibao's integrated pump and exhaust system
Customer Testimonial
Act 1: The Challenge —— Alkaline and Acid Fumes Across the Entire Line
Background
TESB is an electrocoating company in Malaysia. Its pre-treatment production line includes two key processes: Alkaline Degreasing and Pickling, using alkaline degreasing chemicals, hydrochloric acid, and diluted sulfuric acid. Both process lines need pumps to continuously circulate the tank liquid to filter units. At the same time, the workshop requires an exhaust system to send corrosive fumes to a scrubber for treatment.
However, the production line faced a double equipment challenge. On one side, the pre-treatment liquid reaches 53°C, while the alkaline degreaser contains a large amount of oil and sludge. The pickling solution is an 18% mixed-acid solution. The two processes create alkaline vapor and acid mist that spread through the workshop. On the other side, the exhaust system is also exposed to the mixed corrosive environment. Metal fan housings and impellers rusted quickly, while reduced airflow lowered the scrubber's treatment efficiency.
Detailed Pain Points
The customer had reliability problems with both the pumps and fans:
Pump-side problems:
- Alternating acid and alkaline fumes in the workshop attacked horizontal pump motors and bearings, causing frequent electrical failures
- Oil and sludge in the alkaline degreaser, together with corrosive components in the pickling solution, caused both chemical corrosion and organic contamination of wetted parts
- Shaft seals were a weak point, resulting in 2–4 leakage incidents per year
- Average pump life was only 1.5 years, with a total of 12 days of downtime per year
Fan-side problems:
- Metal fans quickly rusted in the mixed acid-alkali fume environment, causing housing and impeller corrosion and deformation
- Airflow gradually decreased, reducing scrubber exhaust efficiency and increasing fume levels in the workshop
- Fan failures caused the production line to slow down or stop, increasing downtime losses
The total annual cost of one complete equipment set reached $850, including purchase, maintenance, and downtime losses.
Highlight Box — Root Cause Analysis
Root Causes
1. Double Corrosion Environment: The production line produces alkaline vapor during degreasing and acid mist during pickling. A single protection method could not handle both environments.
2. Complex Process Liquids: The alkaline degreaser contains oil and sludge, while the 18% mixed acid contains HCl + diluted H₂SO₄. Corrosion and contamination occur at the same time.
3. Weakness of Horizontal Pump Design: The shaft seal was a weak point. Acid and alkaline fumes could affect the seal, causing repeated leakage.
4. Wrong Fan Material: Metal fans quickly rusted in acid and alkaline fumes. As exhaust performance decreased, fume levels increased.
5. Separate Pump and Fan Purchasing: The customer purchased pumps and fans from different brands, resulting in poor system matching and lower overall reliability.
Before Data
Metric | Before Meibao | Impact |
Pump Lifespan | 1.5 years average | Frequent replacement cycle |
Annual Downtime | 12 days/year | ~2.5 production weeks lost |
Leakage Incidents | 2–4 times/year | EHS regulatory risk, safety hazard |
Annual Equipment Cost | $850/set | Purchase + labor + downtime + fan repair |
Medium Concentration | 18% | Mixed HCl + Dilute H₂SO₄ |
Operating Temp | 53°C | Accelerates corrosion and seal wear |
Fan Condition | Metal housing/impeller rusting | Declining exhaust, rising fume concentration |
Act 2: The Solution —— Integrated Pump and Fan Solution
Solution Approach
After studying TESB's actual operating conditions, we found that the customer was facing more than a simple pump replacement problem. The reliability of the pre-treatment line depends on both tank liquid circulation and fume exhaust. If either system fails, the production line may have to stop. More importantly, the workshop contains both alkaline vapor and acid mist at different stages, so all equipment in contact with the process environment needs strong corrosion resistance.
Therefore, we proposed an integrated pump + fan solution:
- MIT-50VK-55NF Vertical Pump: The vertical design keeps the motor above the liquid and away from alkaline and acid fumes. GFRPP wetted parts provide strong resistance to the alkaline degreaser and mixed acid. The seal-less design removes the main source of leakage.
- TF-50C-50HP FRP Centrifugal Fan: The FRP housing and impeller do not rust in mixed acid and alkaline fume environments, helping maintain stable airflow.
The pumps and fans use the same brand and design standards, providing better system matching, simpler after-sales service, and easier maintenance.
Product Selection
Selection Factor | Matching Advantages of MIT-50VK-55NF + TF-50C-50HP |
Vertical Pump Design | Motor stays above the liquid and away from alkaline/acid fumes |
GFRPP Wetted Parts | Glass-fiber reinforced polypropylene provides strong resistance to alkaline degreaser + 18% mixed acid |
Seal-less Design | Removes the shaft seal leakage point and is suitable for liquids containing oil and sludge |
Cavitation Resistance | Submerged impeller installation helps prevent air intake when the liquid level changes |
FRP Fan Material | FRP housing + impeller do not rust in mixed acid and alkaline fumes |
Stable Airflow | Stable exhaust helps maintain scrubber efficiency and workshop conditions |
Integrated Solution | Pumps and fans from one brand, better system matching, and one-stop service |
Highlight Box — Key Technical Advantages
Seal-less Vertical Pumps + Corrosion-Resistant FRP Fans · Complete Line Protection
MIT Vertical Pump Advantages:
· Motor stays away from the liquid and is better protected from alkaline vapor and acid mist
· No mechanical shaft seal, eliminating the main source of leakage
· GFRPP wetted parts provide strong resistance to degreaser and mixed acid
· Submerged installation helps prevent air intake and cavitation when the liquid level changes
TF FRP Fan Advantages:
· FRP housing + impeller do not rust in mixed acid and alkaline fumes
· Stable airflow helps maintain scrubber treatment efficiency
· Same-brand design provides better system coordination
Integrated Value: Pumps + fans from one supplier, with unified installation and after-sales service, so the customer does not need to deal with multiple suppliers.
Specification Table — Pump
Specification | Selected Model (MIT-50VK-55NF) | Key Benefit |
Wet-End Material | GFRPP (Glass-Fiber Reinforced Polypropylene) | Corrosion-resistant to alkaline degreaser + mixed acid |
Drive Type | Vertical direct drive | No shaft seal, zero leakage |
Max Flow | 520 L/min | Stable circulation to filter units |
Max Head | 27 m | Handles system back pressure |
Motor Rating | 3.75 kW | Adequate power with good energy efficiency |
Units Installed | 3 units | Full coverage for degreasing + pickling lines |
Sealing | Seal-less (vertical submerged) | No seal wear, no leakage |
Specification Table — Fan
Specification | Selected Model (TF-50C-50HP) | Key Benefit |
Housing Material | FRP (Fiber-Reinforced Plastic) | No rust in mixed acid-alkali fumes |
Impeller Material | FRP (Fiber-Reinforced Plastic) | Maintains balance without corrosion deformation |
Application | Exhaust to scrubber system | Stable airflow for fume treatment |
Units Installed | 3 units | Matched to pump stations |
Corrosion Resistance | Alkaline vapor + acid mist | Suitable for mixed environments |
Project Timeline
Stage | Milestone | Description |
Application Assessment | Week 1–2 | On-site review of the degreasing/pickling lines, exhaust system, and scrubber requirements |
Custom Production | Week 3–5 | 3 pump sets + 3 fan sets customized to customer connections and fully inspected before shipment |
Installation & Commissioning | Week 6–7 | Pump installation, duct connection, system testing, and loaded trial operation |
Stable Operation | Month 16+ | Continuous no-failure operation to date, with ongoing follow-up |
Act 3: The Result —— 16+ Months of Zero Leakage and Zero Downtime
Results
Since installation and commissioning were completed in April 2025, three MIT-50VK-55NF vertical pumps and three TF-50C-50HP FRP fans have operated on TESB's electrocoating pre-treatment line for more than 16 months. During this period, all equipment has achieved zero leakage and zero downtime:
- Pump side: Even with oil and sludge in the degreasing tank and an 18% mixed-acid solution in the pickling tank, the vertical pumps have maintained a stable flow of 520 L/min, keeping the circulation and filtration process running without interruption. The seal-less design has eliminated leakage on the workshop floor.
- Fan side: The FRP fans have operated in the mixed acid and alkaline fume environment for 16 months without visible rust. Airflow has remained stable, helping the scrubber maintain its treatment efficiency and improving workshop air conditions.
Director Daniel specifically noted that other pump brands used in the past required frequent maintenance, while Meibao pumps greatly reduced maintenance interruptions. The integrated pump and fan solution has helped the entire pre-treatment line run reliably over the long term.
Results Cards
✓ | $ | 🛡️ |
16+ mo | $500 | 0 |
Zero-downtime continuous operation | Annual cost saving vs. previous equipment | Leakage incidents across all units |
Before vs After Comparison
Comparison | Before (Previous Equipment) | After (MIT-50VK-55NF + TF-50C-50HP) | Improvement |
Corrosion | Pump corrosion and replacement after 1.5 years; metal fan parts rusted and deformed | GFRPP/FRP equipment operated for 16 months without corrosion | 2–3× longer service life; no fan rust |
Leakage Incidents | 2–4 times/year | 0 times | Leakage eliminated |
Production Downtime | 12 days/year | 0 days | 2.5 weeks of production recovered |
EHS Compliance | Frequent leakage + acid mist buildup, high environmental risk | Dry workshop floor + stable exhaust, supporting compliance | Major reduction in risk |
Annual Total Cost | $850/set (including pump + fan + maintenance + downtime losses) | Initial investment only, with very low operating costs | $500+/set annual saving |
Recommended Pumps for
Complete Pre-Treatment Solution: MIT Vertical Pumps + TF FRP Fans Deliver 16+ Months of Zero-Leakage, Zero-Downtime Operation
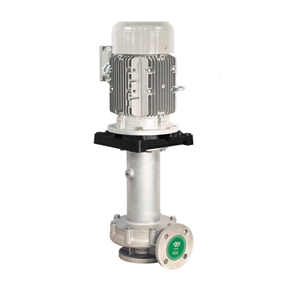
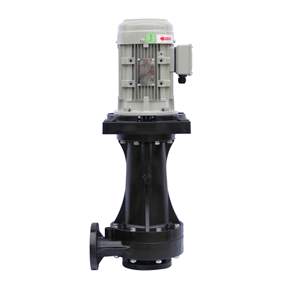
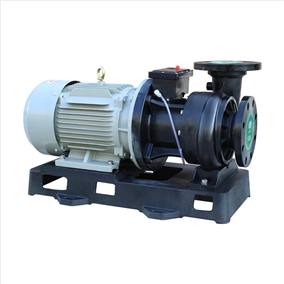
Each pump model is available in multiple material configurations to match the exact chemical and thermal requirements of your process.
 Recommended
 Recommended
 Recommended
 Recommended
Related Case Studies
Get a Free Technical Proposal
Tell us about your HF acid, chemical, or corrosive media application. Our engineering team will recommend the right pump and provide a detailed proposal within 48 hours.
 WhatsApp
 Facebook
 LinkedIn
 YouTube
